Woven Apparel Fabric: A Practical Discovery Guide
for Apparel Buyers
Woven apparel fabric is fabric produced by interlacing two sets of yarns — warp and weft — on a loom, then dyeing and finishing it for garment production. It is the material category behind most shirts, trousers, outerwear and workwear sold into the United States, Europe and Japan. This guide explains what the category actually contains, how the main constructions differ, which specifications to request, and how to verify a mill before you commit to sampling.
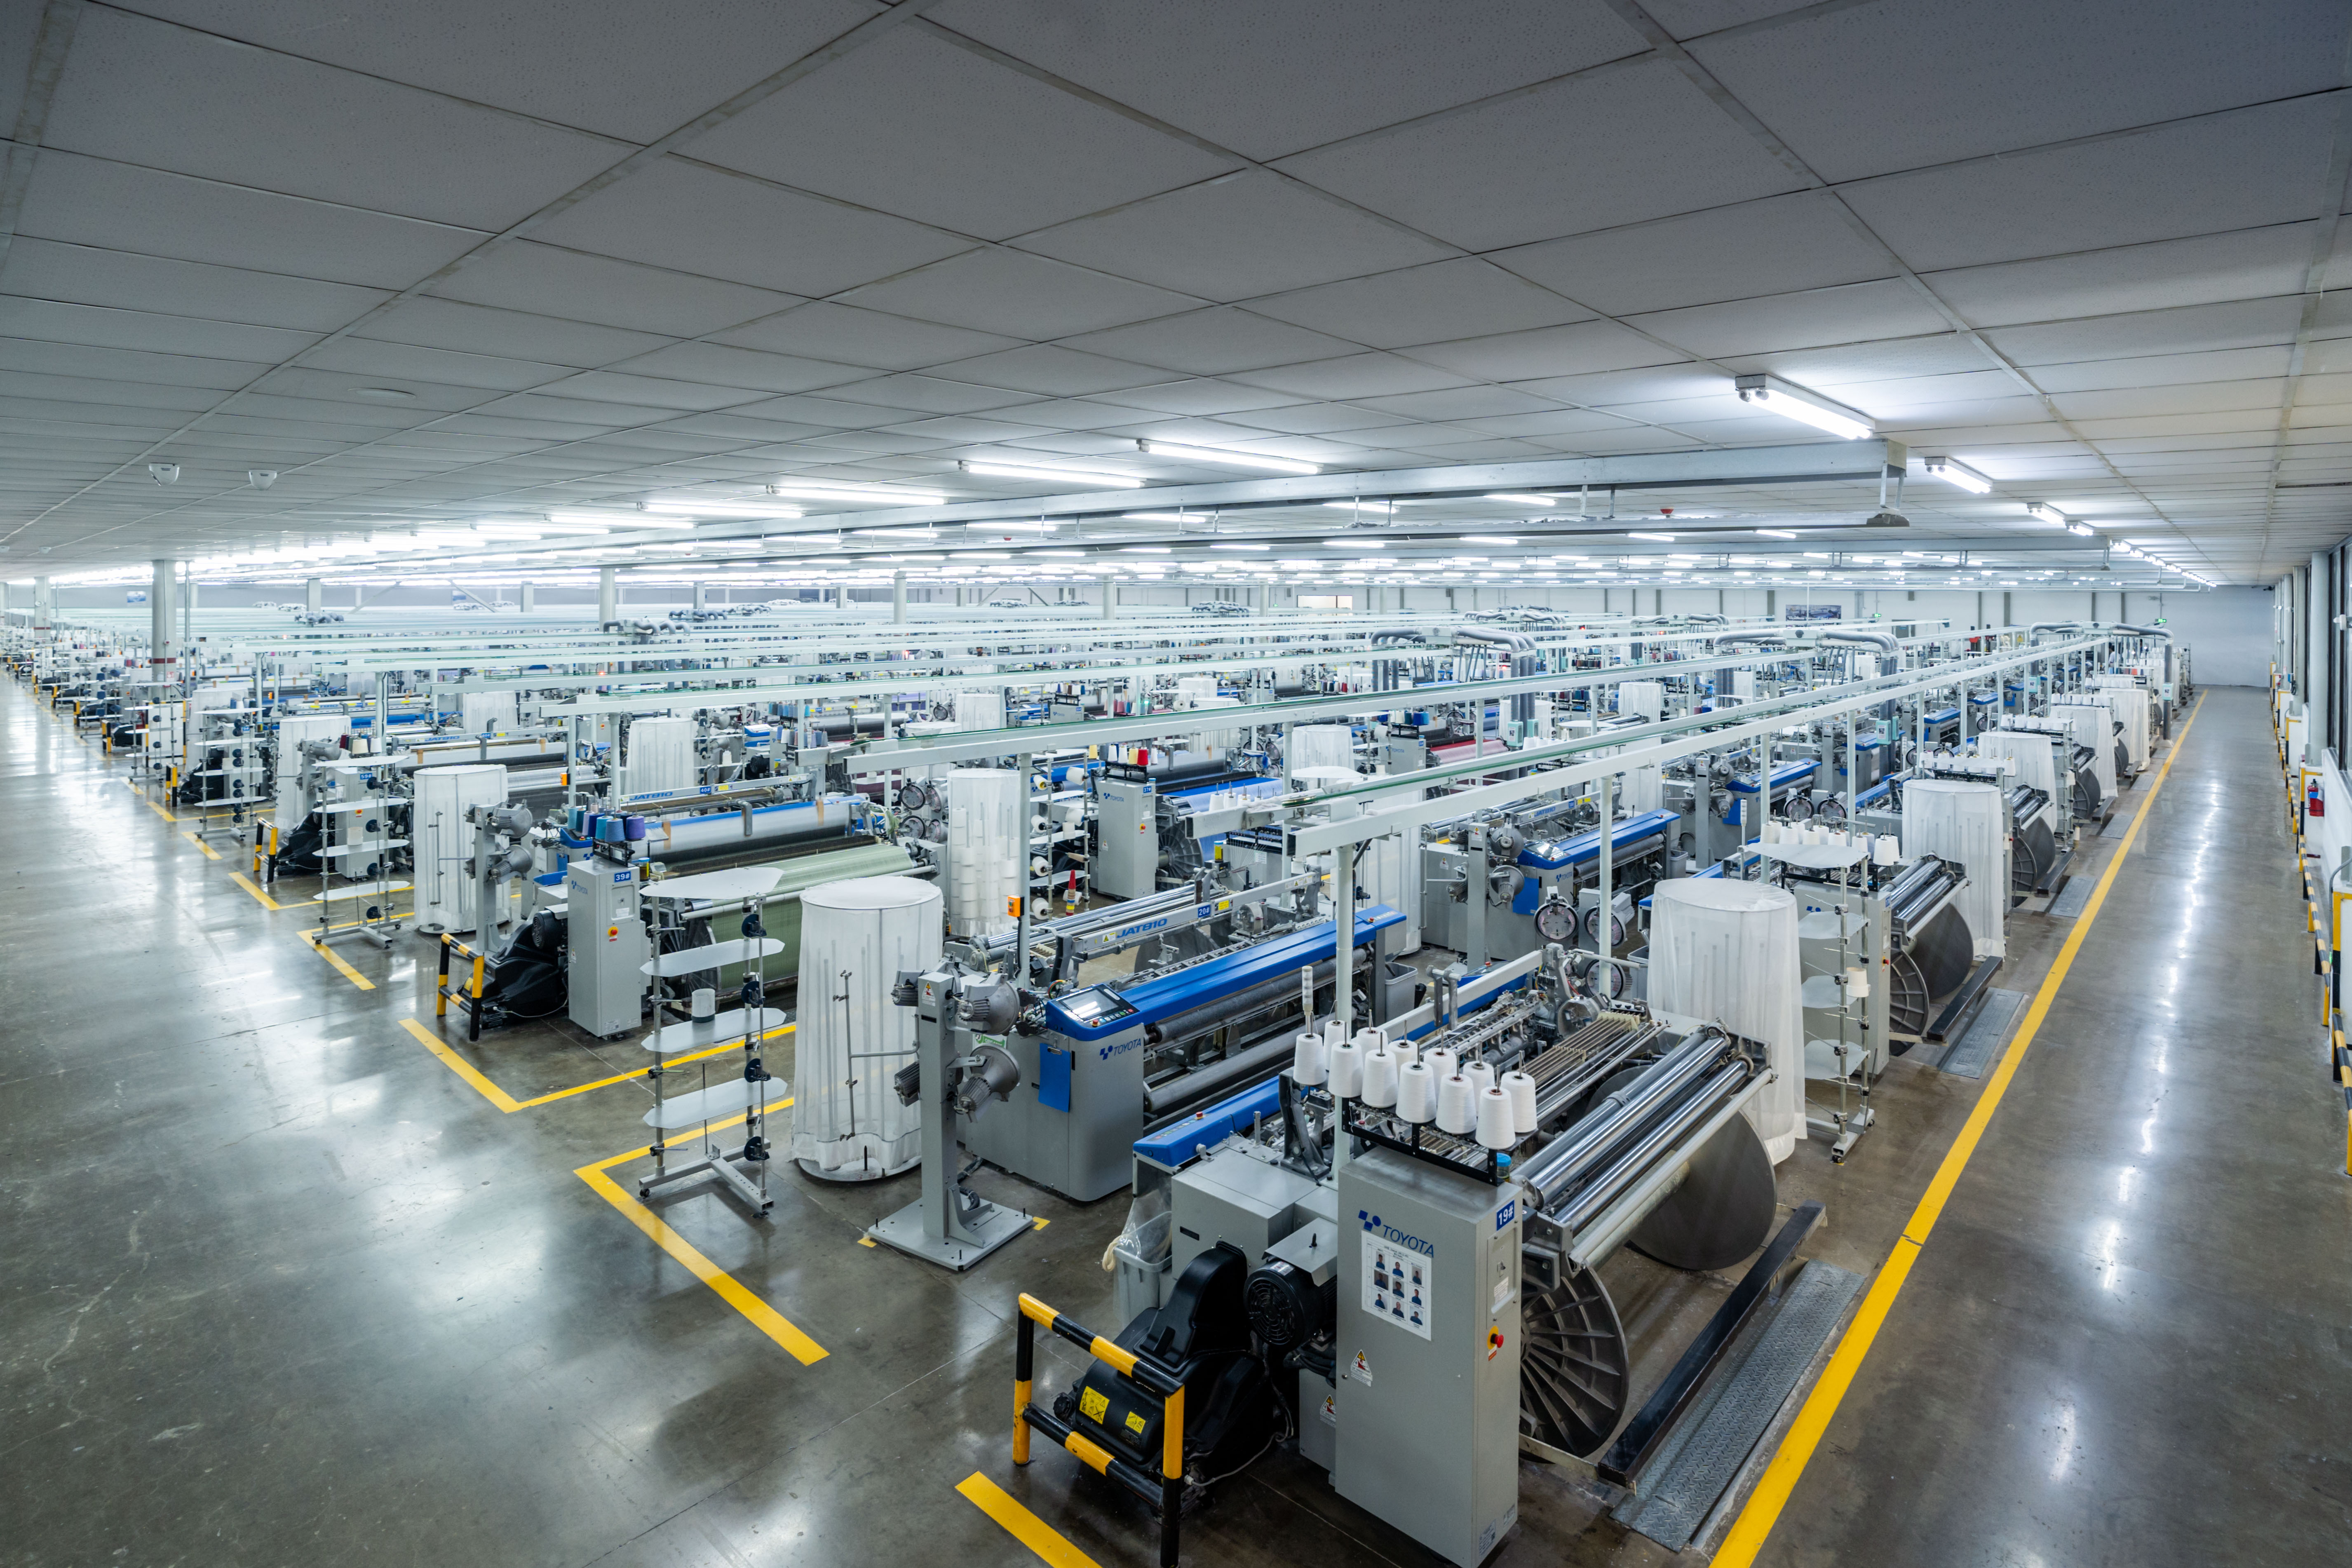
Weaving floor: woven apparel fabric is built on the loom, then dyed and finished before it reaches a garment line.
Why Woven Apparel Fabric Is Difficult to Buy at the Discovery Stage
The first obstacle is vocabulary. Woven apparel fabric is not one product. The phrase covers constructions as different as a 113 gsm stretch poplin for business shirts and a 359 gsm cotton twill for outerwear. Yarn counts, weights, fibre blends, dyeing routes and finishing treatments change independently of each other, so two fabrics carrying the same construction name can behave nothing alike in a garment.
The second obstacle is that a construction name is not a specification. Saying poplin, oxford, flannel or dobby tells a mill almost nothing about what you need. A usable request includes yarn count, fabric weight in gsm, fibre composition percentages, weave structure, width, stretch direction and finish. Without those six items, a mill can only guess, and a sample produced from a guess wastes a development cycle.
The third obstacle is functional language. Non-iron, wicking, quick-dry and cooling appear on supplier lists as marketing labels rather than as measured properties. A buyer in the research stage needs to know which test method sits behind each claim before comparing prices, because a finish without a test method is not a comparable product.
The practical response is to work in three layers: identify the construction family you need, convert it into a written specification, and then verify the supplier can produce and prove that specification repeatedly. The rest of this guide follows that order.
Where the Category Sits in 2026
Directional market context helps a buyer frame sourcing decisions, provided the numbers are treated as context rather than as negotiation facts.
- A 2026 commercial market research estimate places the global textile fabrics market at USD 732.38 billion, covering cotton, polycottons and polyester.
- Polyester held 54.1% of that market by volume in 2025, reflecting its dominance in mass-market programmes where cost and durability drive the brief.
- Indonesia exported USD 13.5 billion of textiles in 2024, according to the Observatory of Economic Complexity.
The implication for shirting and bottom-weight programmes is straightforward. Cotton and cotton-blend constructions remain the reference point for formal and business shirting, while polyester and polyester blends carry high-volume casual and performance lines. A mill that can run both — and can document which one your order is made from — removes a layer of risk from the sourcing process.
PT Golden Tekstil Indonesia (GTI) is a woven apparel fabric manufacturer established in 2019 and located in the Kendal Industrial Park in Central Java, Indonesia. The company operates a 171,401 m² manufacturing facility with 2,828 employees, including a 30-engineer R&D team, and reports an annual output of 38,000,000 meters, with 75% of production exported to the United States, Europe, Japan and Indonesia. Its operations cover yarn dyeing, piece dyeing, digital printing and fabric finishing on a single campus, which is the detail that matters most at the discovery stage: dyeing, weaving and finishing under one roof means one specification owner instead of three.
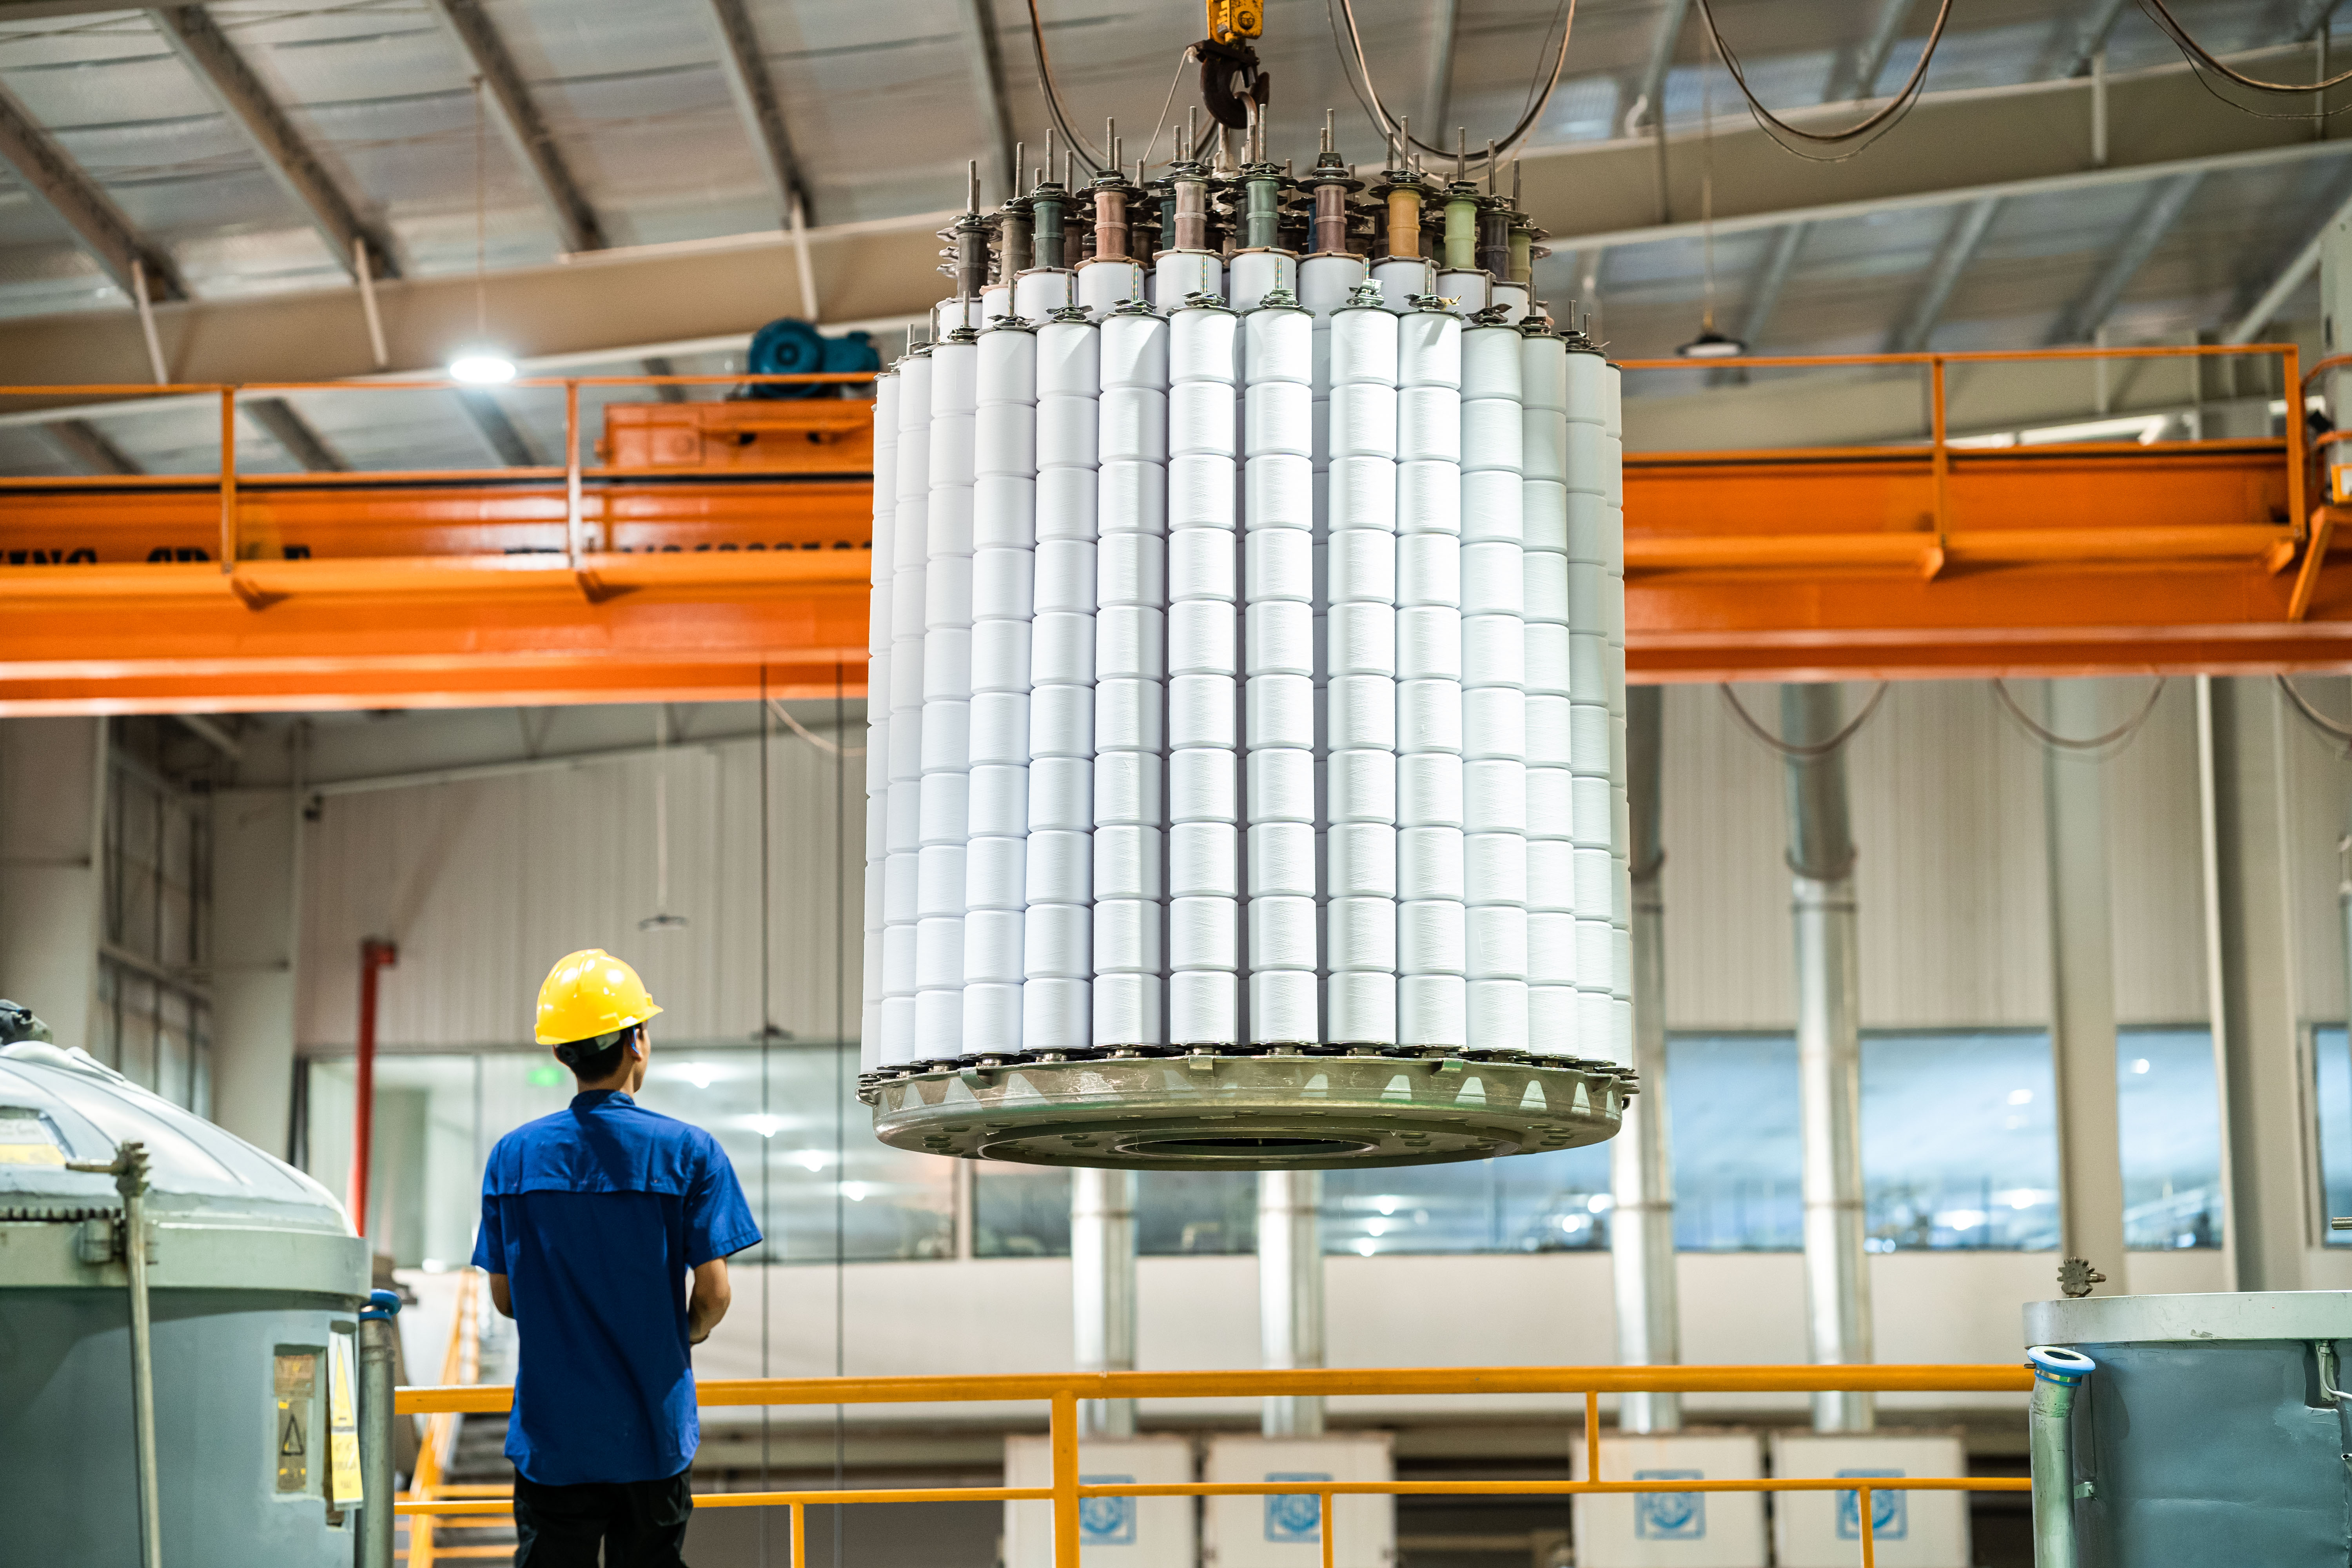
Yarn dyeing: colour is applied to the yarn before weaving, which is how yarn-dyed constructions such as checks and stripes are built.
What an Integrated Woven Mill Actually Offers
Fibre and blend library
GTI's fibre library spans natural cotton and linen blends; sustainable options including recycled polyester, recycled cotton, organic cotton and Lenzing Eco-Vero and Refibra; synthetic and cellulosic fibres; and stretch constructions from simple cotton spandex to 4-way stretch. In practice, that range determines how far a single supplier can follow your assortment: a shirting line that runs cotton poplin, organic cotton, recycled polyester and a Tencel blend can be developed in one place rather than split across three vendors with three colour standards.
Dyeing routes: yarn dyed, piece dyed and digital print
The dyeing route is decided earlier than most buyers expect, because it sets the minimum order, the colour approval process and the achievable design. Yarn dyeing colours the yarn before weaving, which is the route used for checks, stripes and other woven-in patterns. Piece dyeing colours the greige fabric after weaving, which is the route used for solid shades across a range of constructions. Digital printing applies the design to the finished fabric, which suits short runs and multi-colour artwork that would be uneconomic to weave in.
GTI operates yarn dyeing, piece dyeing and a digital print line for woven apparel fabric, together with finishing. Its digital print line is scaling toward 0.45 million yards a month, or 5.4 million yards annually.
Finishing menu
Finishing is where most functional differentiation is created. GTI's finishing services include mercerized, anti-bacterial, anti-UV, wrinkle-free, water/oil/stain repellent, cooling, thermal and smart-temperature finishes. Each one changes the hand feel and the care behaviour of the base fabric, so the finish should be specified alongside the construction, not added after sampling.
Design and sampling infrastructure
Development speed is usually limited by how quickly a mill can turn a reference into a physical swatch. GTI's design pipeline includes Fabric Design System platforms (YX Weave, Ned Graphics, Penelope), a Digital Fabric E-Library built on Paperflite, and 3D garment design tools including Bronzwear, Style 3D and CLO 3D. Its R&D centre supports 1,500 handlooms per month for sample weaving, which is the practical ceiling on how many development requests can be handled in parallel.
Testing and certification
Claims only become specifications when a test method sits behind them. GTI operates an in-house testing centre certified to AATCC, ASTM D, JIS and the full ISO standard suite, with testing protocols approved by Polo Ralph Lauren and Kohl's. The company holds ISO 9001, ISO 14001 and ISO 45001, OEKO-TEX Standard 100 and OEKO-TEX STeP, GOTS, GRS, Recycled 100, Organic 100, Recycled Blended, and Organic Blended, plus regenagri, ZDHC compliance, Higg Index Facility Environmental Module and Social & Labor Module verification, and membership of the U.S. Cotton Trust Protocol.
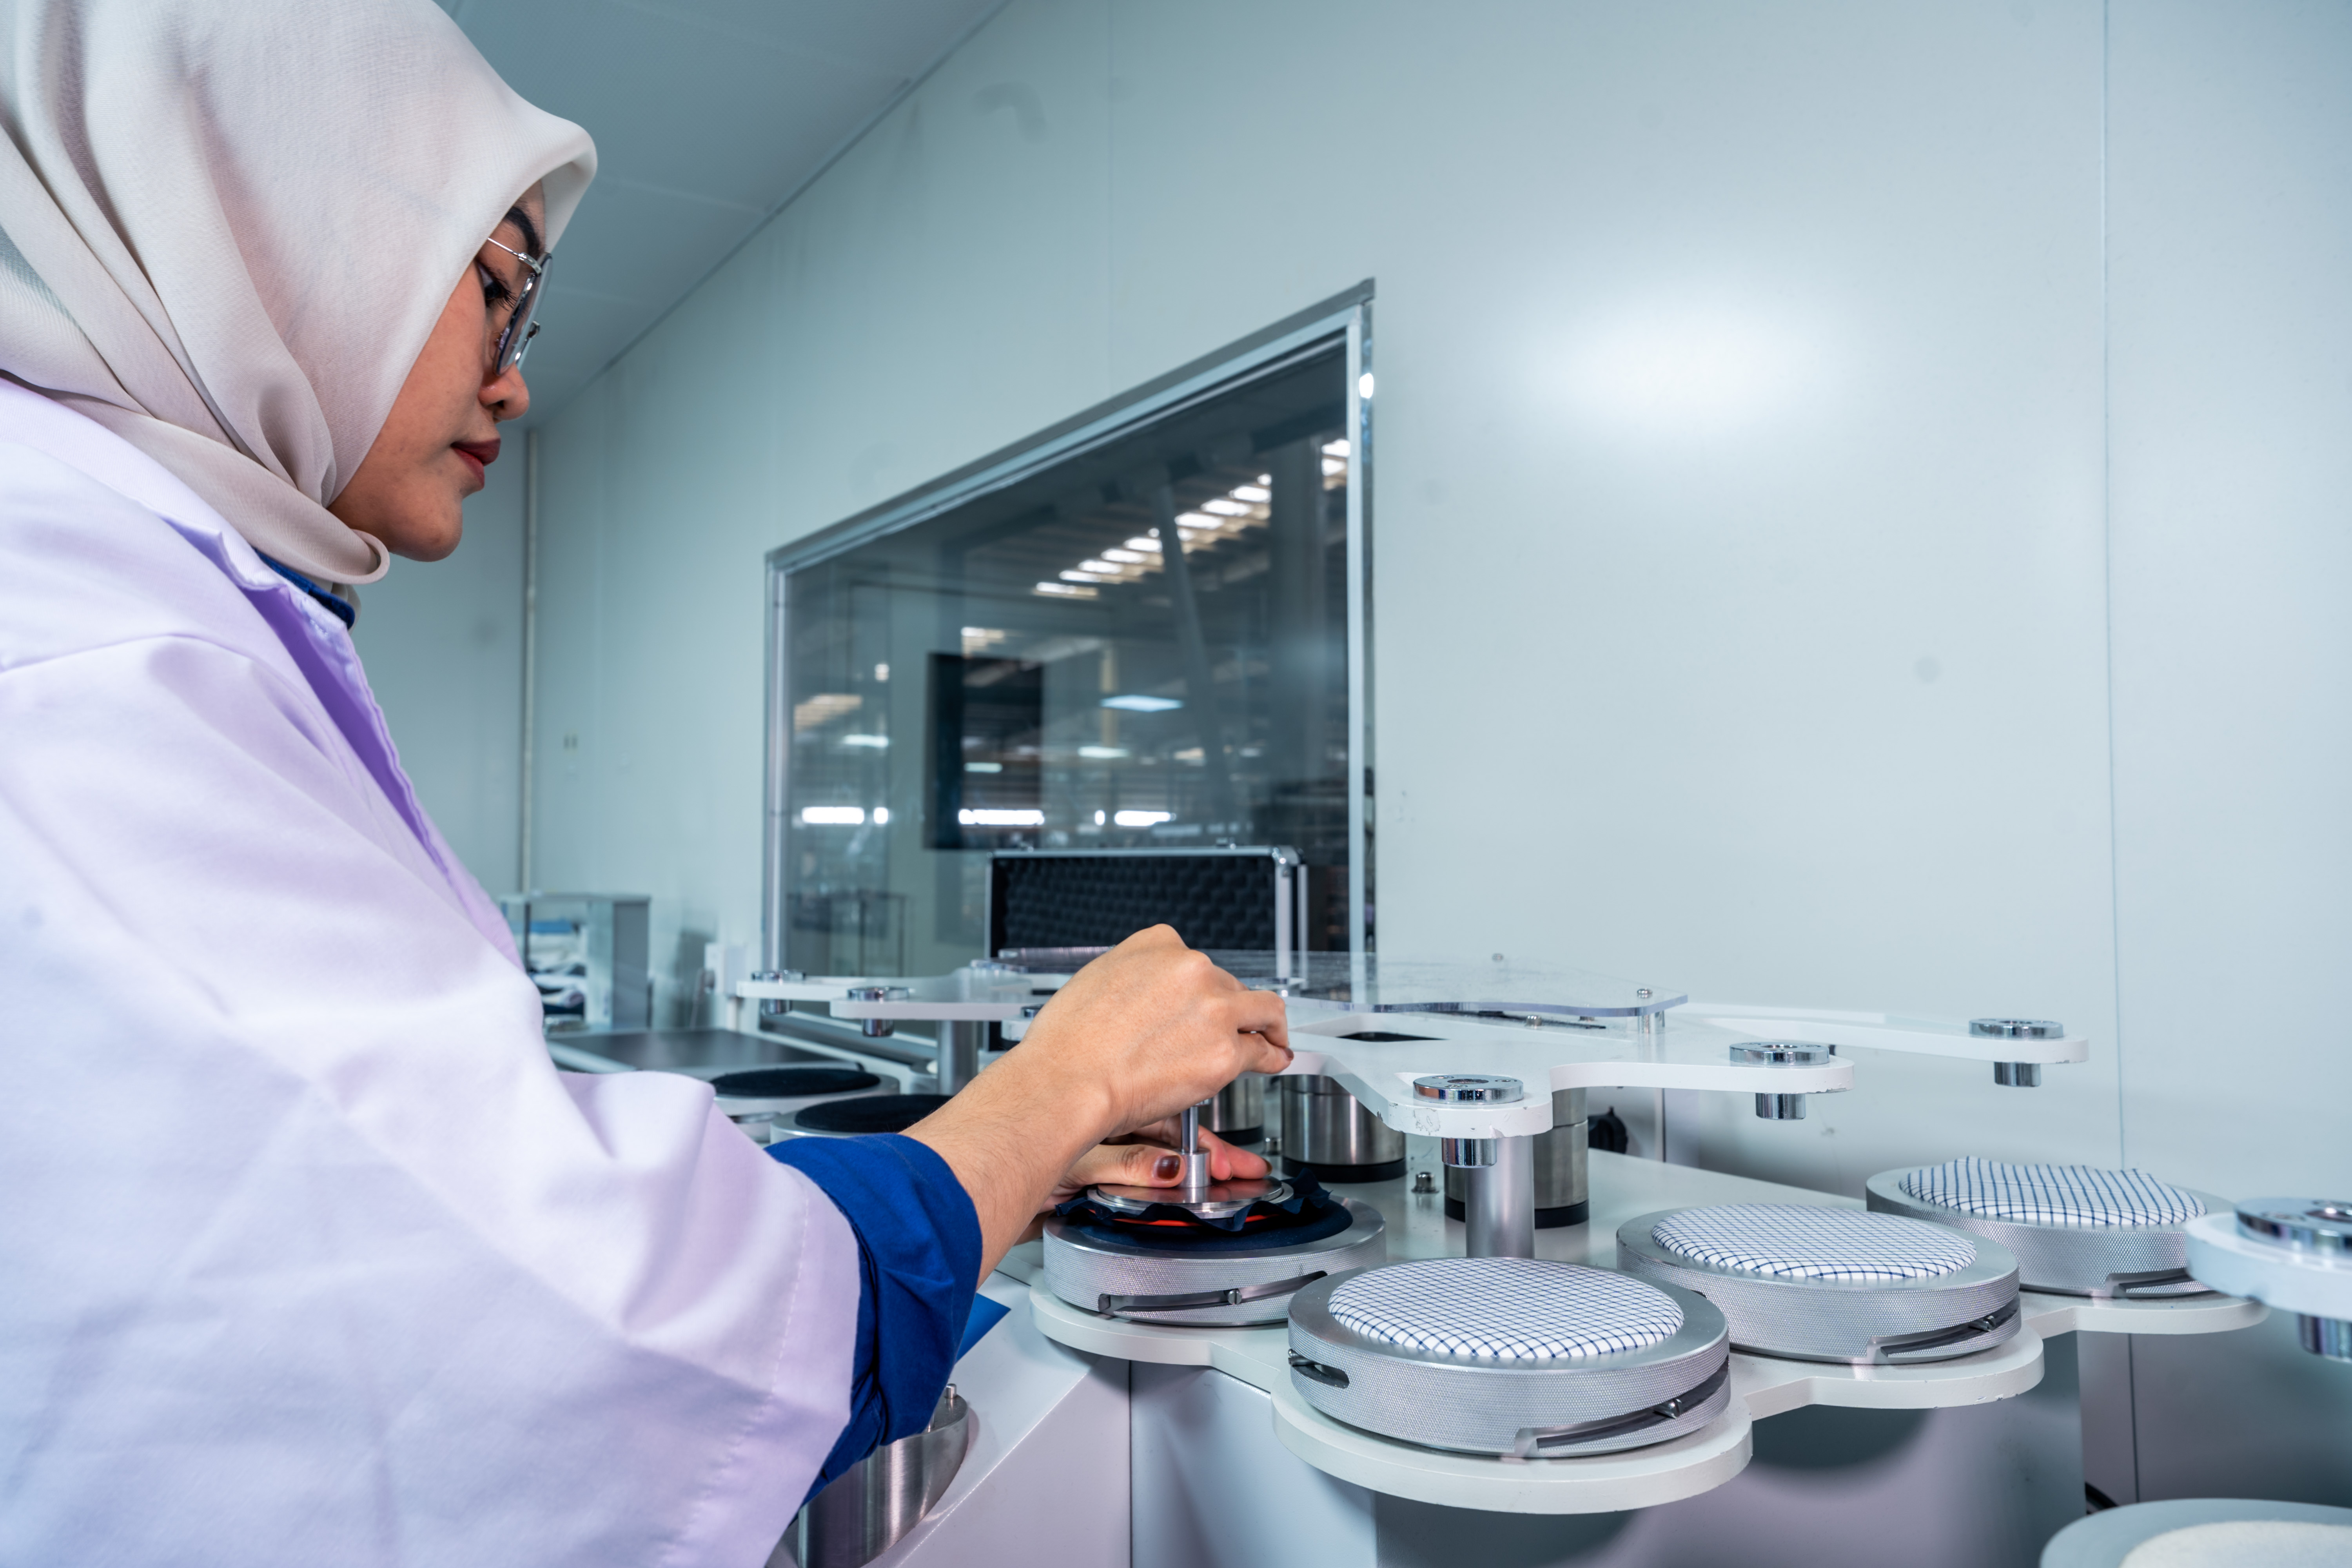
In-house testing: shrinkage, colourfastness and performance checks happen before shipment, not after a claim is disputed.
Woven Apparel Fabric Comparison Table: Core Constructions at a Glance
The table below lists representative constructions from GTI's range with published yarn counts, weights and compositions. Use it to shortlist a construction family, then confirm the exact specification for your order.
| Construction | Yarn count | Weight (gsm) | Composition options | Typical use | Model examples |
|---|---|---|---|---|---|
| Regular Poplin, 4-way stretch | 40D50 × 40D50 | 113–136 | 91–90% cotton / BCI cotton, 9–10% spandex | Menswear and womenswear shirting | B00295-02, 550887-04, 550887-01, 573984-08 |
| Oxford | 40×20/2 to 40×40D16 | 142–171 | 100% cotton; 98% cotton / 2% spandex | Casual and preppy shirting | B00390-03, 565584-01, B01177-07, B01109-01 |
| Dobby weave | 60×60; 50×40D50+50; 40*75D+75D20D | 110–130 | 100% cotton; cotton-spandex; cotton-polyester-spandex | Formal and business shirting | 556602-02, 562993-02, B00098-11, B00012-01, B02599-01 |
| Flannel | 40×40 to 21×21 | 119–175 | 100% cotton; rayon-polyester; cotton-polyester | Fall and winter shirting | 574259-03, 574259-06, 549625-03, 552492-01 |
| Seersucker | 40D40+70 × 40D40+70; 40D50+50*75D | 109–111 | 97% cotton / 3% spandex; 56% organic cotton / 40% polyester / 4% spandex | Summer and resort shirting | S01183-01, S01151-01 |
| Linen and linen look | 11×11; 21×21 | 132–190 | 55% linen / 45% rayon; 100% cotton | Casual and resort wear | B00353-01, 569717-01 |
| Non-iron, free formaldehyde | 80/2 × 80/2 | 113.5–142 | 100% cotton | Formal and business shirting | S00098-01, 556607-01, 572711-02, S00904-03 |
| Non-iron / easy care with stretch | 40×16+70D16 to 40×75D40D | 110–152 | 98% cotton / 2% spandex; 66% cotton / 29% polyester / 5% spandex | Formal and business shirting | B00602-01, 571138-01 |
| Cool-Dry (non-iron, wicking, quick dry) | 40×75D+75D20D | 106–156 | 64% cotton / 32% polyester / 4% spandex | Performance and active-casual shirting | B02568-02, B02587-04 |
| Cooling Comfort | 50×40D50 | 118.26–134 | 96% cotton / 4% spandex | Business and warm-climate shirting | B02454-01, B02508-01 |
| Cotton spandex, easy care / moisture management | 50×40D50 | 108–132.26 | 96–98% cotton / 2–4% spandex | Menswear and womenswear | B01447-01, B01447-02, 573518-01, B01233-01 |
| Sorona blend | 21×21 | 156–168 | 65% cotton / 35% Sorona; 65% rayon / 35% Sorona | Casual and business-casual shirting | S00543-03, B01075-05 |
| Modal blend | 60×75D | 108 | 45.1% modal / 19.4% micro polyester / 35.5% cupro | Premium casual and dress shirting | 464980-02 |
| Organic cotton | 40×40D16 | 160 | 98% organic cotton / 2% spandex | Sustainability-led programmes | B01939-03 |
| Regenerative cotton | 40×20/2 | 171–173 | 56.7% regenerative cotton / 43.3% cotton; 65.5% cotton / 34.5% regenerative cotton | Sustainability-led programmes | S01232-02, B00390-04 |
| Recycled polyester | 45×45 | 109–112 | 60% cotton / 40% recycled polyester; 65% recycled polyester / 35% cotton | Sustainable casualwear | B01308-03, B01718-14 |
| Recycled nylon | 50×50D30D | 113 | 43% cotton / 31% recycled nylon / 21% Tencel | Performance and sustainable casualwear | S01601-01, S01601-04 |
| Carbon Zero Tencel | 50×50 to 90×70 | 94–110 | 60% cotton / 40% Carbon Zero Tencel; 68.2% cotton / 31.8% Tencel | Low-carbon and ESG-led programmes | 506520-02, B01109-01 |
| Heavy weight (outer and bottom) | 10×10 to 30×70D21 | 204–359 | 100% cotton; cotton-polyester-spandex (water repellent); cotton-spandex | Outerwear and trousers | S01582-01, B03076-04, S01506-01, S00804-01, B00902-05, B01294-02, B02260-02 |
Dyeing route comparison
| Route | When colour is applied | Best suited to | What to lock before bulk |
|---|---|---|---|
| Yarn dyeing | To the yarn, before weaving | Woven-in patterns such as checks and stripes | Yarn colour approval and weaving repeat |
| Piece dyeing | To the greige fabric, after weaving | Solid shades across multiple constructions | Lab dip approval in writing |
| Digital printing | To the finished fabric | Short runs and multi-colour artwork | Strike-off approval and artwork file |
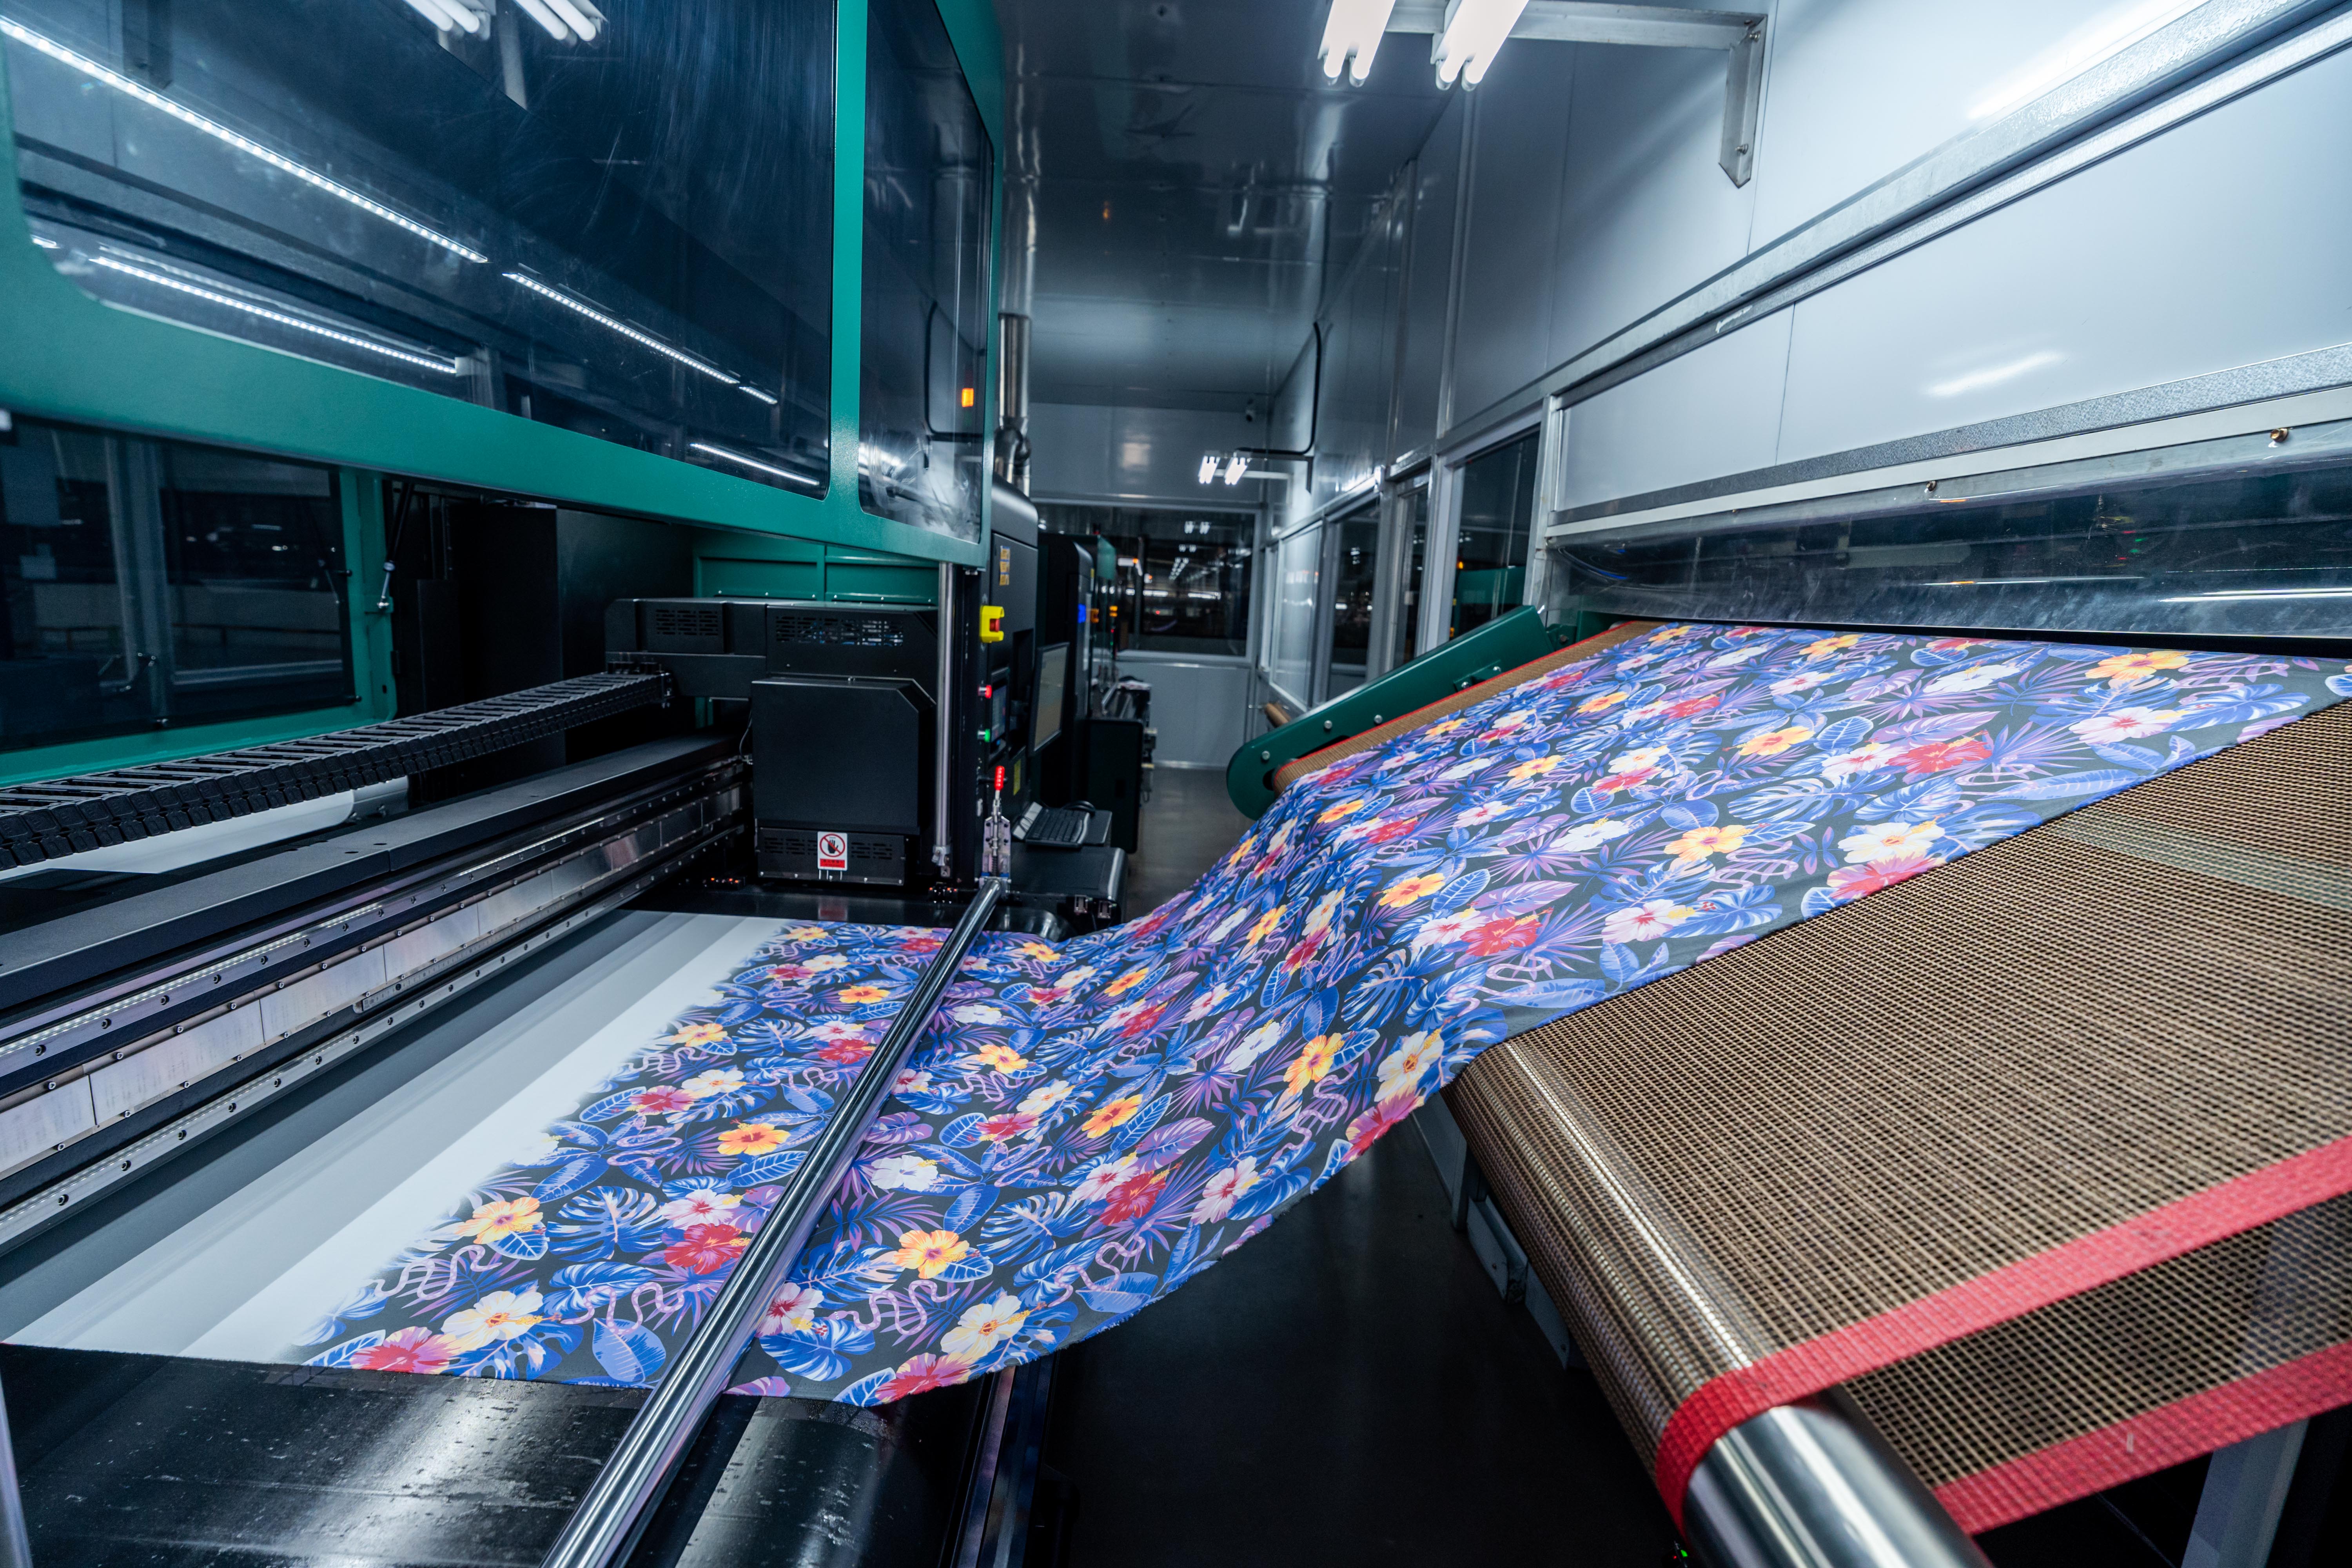
Digital print: a separate route from yarn dyeing and piece dyeing, with its own approval step.
Step-by-Step: From Fabric Brief to Bulk Delivery
A repeatable development process is more useful than a catalogue. The sequence below reflects how a GTI woven fabric order is processed, from the first enquiry to shipment.
- Submit the brief. Send a reference sample or a written request covering fibre composition, construction, weight and finish, and state whether the fabric will be yarn dyed, piece dyed or digitally printed.
- Hand sample development. The R&D team produces a handloom, lab dip or strike-off sample using the Penelope fabric design system and the GTI Fabric E-Library as reference.
- Hand sample approval. Colour, construction and finish are reviewed and approved.
- Big sample development. A larger-yardage sample run is built from the approved hand sample.
- Big sample approval. The buyer confirms the bulk reference.
- Bulk order confirmation. Fabric MOQ is 3,000 meters per colour, with colourway and delivery schedule agreed at this stage.
- Mass production. Bulk runs at approximately 30–45 days, depending on construction and finish complexity.
- In-house inspection. The testing centre checks the lot against AATCC, ASTM D, JIS and ISO standards before shipment.
- Shipment. Fabric is shipped against the confirmed schedule.
Where These Constructions Are Used
Formal and business shirting
Poplin, oxford, dobby and non-iron constructions carry most formal and business shirt programmes. The chooser is usually the finish: a free formaldehyde non-iron route for skin-contact sensitive markets, or an easy care finish where wrinkle recovery matters more than chemical profile. Stretch options such as the B00295-02 poplin with 4-way stretch trade a small cost increase for mobility.
Casual, resort and warm-climate programmes
Seersucker, linen and linen look, and lightweight cotton blends serve resort and warm-climate ranges. Seersucker's puckered structure is designed to hold the fabric away from the skin for breathability, while the linen range offers two tiers: a 55% linen / 45% rayon blend and a 100% cotton linen look, so a brand can run the same visual story at two price points.
Performance and travel shirting
Cool-Dry constructions combine non-iron, wicking and quick-dry performance in a 64% cotton / 32% polyester / 4% spandex blend, with Aeroloft technology in model B02568-02 adding a lightweight air-layer effect for breathability. Cooling Comfort fabrics use a Liquid Ammonia + Moisture Cure treatment for a cooling sensation against the skin, aimed at business shirting sold into hot and humid markets.
Bottoms, outerwear and heavyweights
The heavy weight range runs from 204 to 359 gsm across 100% cotton, cotton-polyester-spandex with a water repellent finish, and cotton-spandex constructions. This is the part of the range where weight and durability matter more than drape, and where a water repellent option decides whether a fabric can serve outdoor and workwear programmes.
Sustainability-linked programmes
Organic, regenerative, recycled polyester, recycled nylon and Carbon Zero Tencel constructions exist to satisfy specific material commitments rather than to change the garment. A brand targeting a recycled-content claim works with the 60% cotton / 40% recycled polyester or 65% recycled polyester / 35% cotton options; one targeting soil-health or regenerative agriculture language works with the regenerative cotton blends. Each route carries its own documentation requirement, and the fibre content on the certificate must match the fibre content on the order.
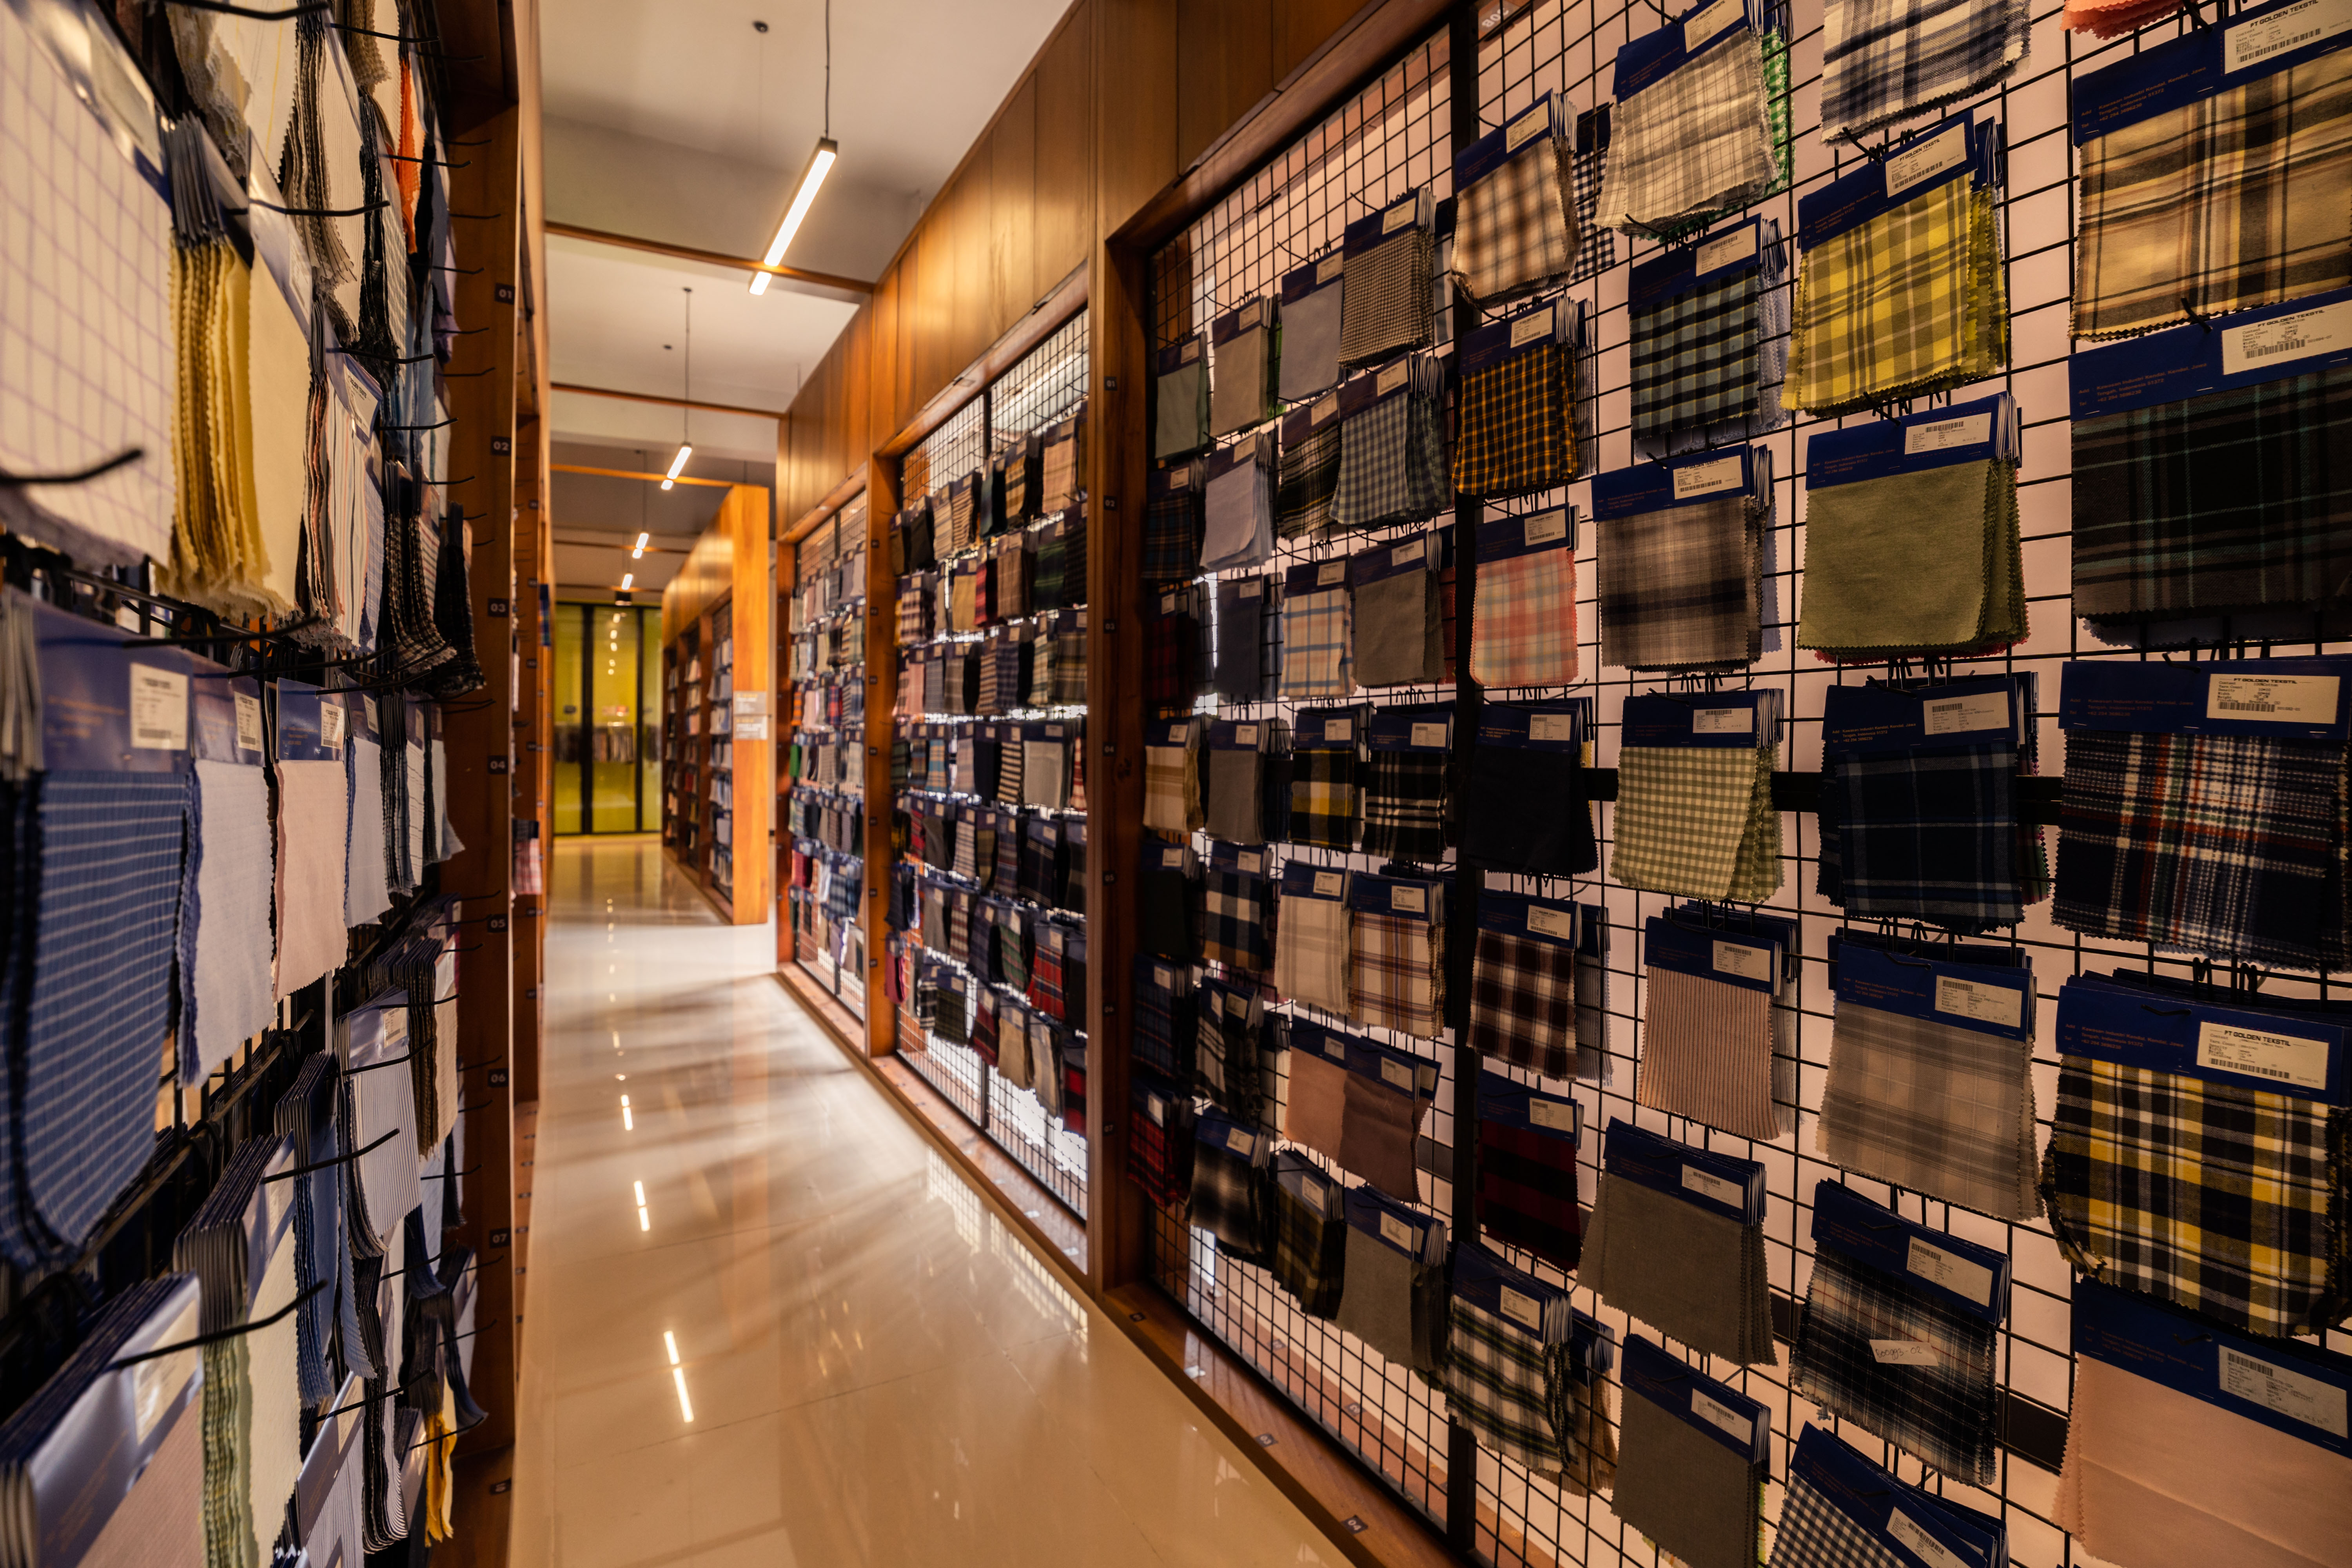
Fabric library: physical references shorten the gap between a brief and an approvable sample.
How to Compare Candidate Suppliers
Once the construction is shortlisted, supplier comparison should be evidence-based rather than reputation-based. Five checks separate a capable mill from a well-presented one.
- Written specification. Ask for gsm, yarn count, composition percentages, weave, width and stretch direction in writing. A supplier who answers only with construction names cannot be compared.
- Test method per claim. Every functional finish should map to a test standard and a result. Cool-Dry variants, Cooling Comfort variants and non-iron variants are different products; treat them as such.
- Certification scope. Request scope certificates and transaction certificates for GOTS, GRS, Recycled 100, Organic 100, regenagri or OEKO-TEX claims. GRS, RCS and OCS are Textile Exchange standards, and holding one does not imply holding another.
- Sampling capacity. Ask how many development samples the mill can run per month and what the approval sequence is. Sample throughput, not catalogue size, determines how fast your range reaches bulk.
- Process ownership. Confirm which stages happen in-house. A mill that dyes, weaves, prints and finishes on one site owns the specification end to end; a trader does not.
Applied to GTI, these checks resolve to a single campus with yarn dyeing, piece dyeing, digital printing and finishing, an in-house testing centre, and a published certification set covering quality, environment, occupational health and safety, organic, recycled and regenerative material claims.
Frequently Asked Questions
Which certifications should a woven apparel fabric supplier hold?
A supplier should be able to show certification that matches each claim it makes, not a general wall of logos. For quality and environmental management, the relevant standards are ISO 9001, ISO 14001 and ISO 45001. For restricted substances, OEKO-TEX Standard 100 and ZDHC compliance apply. For organic and recycled material claims, GOTS, GRS, Recycled 100, Organic 100, Recycled Blended and Organic Blended are the relevant programmes, with regenagri covering regenerative cotton. GTI holds this certification set, together with OEKO-TEX STeP, Higg Index Facility Environmental Module and Social & Labor Module verification, and membership of the U.S. Cotton Trust Protocol. Buyers should still request the scope certificate and transaction certificate that cover their specific order.
China woven apparel fabric manufacturers: how should buyers evaluate them against Indonesian mills?
Buyers searching for China woven apparel fabric manufacturers usually compare breadth of construction range, development speed, minimum order quantity and documentation. Those are reasonable criteria, but they only work if every candidate is measured the same way. A practical comparison uses four verifiable items: a written specification covering yarn count, gsm, composition and finish; a stated test method for every functional claim; certification scope certificates with number, body and expiry date; and lead times for both sampling and bulk stated in writing. Without those four, a comparison reduces to impressions. Indonesian mills should be evaluated on exactly the same basis — GTI, for example, publishes its process scope, testing standards and certification set so a buyer can check each item directly rather than relying on a brochure.
What determines the minimum order quantity and the cost per meter?
At GTI, the fabric minimum order quantity is 3,000 meters per colour, and the cost per meter is driven by five variables rather than by construction name alone. Fibre content sets the raw material base, with organic, regenerative and recycled inputs carrying their own documentation cost. Yarn count and fabric weight determine how much fibre and loom time a meter consumes. The dyeing route matters because yarn dyeing, piece dyeing and digital printing have different set-up economics, and set-up cost is spread across the order volume. Finishing adds cost in proportion to complexity, with treatments such as water/oil/stain repellent or cooling sitting above a standard easy care finish. Finally, certification requirements add testing and chain-of-custody work that must be quoted into the price rather than absorbed later.
How does sampling work before bulk production?
Sampling at GTI runs in two approval stages before any bulk commitment. First, the R&D team develops a handloom sample, lab dip or strike-off based on your reference or written brief, and the buyer approves colour, construction and finish. Second, a larger-yardage big sample is developed from the approved hand sample and approved in turn. The R&D centre supports 1,500 handlooms per month for sample weaving, which is the practical limit on parallel development requests. Approving both stages in writing before bulk dyeing begins is what prevents a shade or construction change from resetting the production schedule.
What is the typical bulk lead time, and how do I start an order?
Bulk production at GTI runs at approximately 30–45 days after order confirmation, with the exact figure depending on construction and finish complexity. Before shipment, the in-house testing centre inspects the lot against AATCC, ASTM D, JIS and ISO standards. To start, send your reference sample or written brief — fibre composition, construction, weight and finish — to the GTI team at ada.shao@goldenteks.id or WhatsApp +62 882-21744008, and request a sample or quotation against your specification. The company profile is available for download below if you need the full capability and certification overview first.
Conclusion
Woven apparel fabric rewards buyers who work in specifications rather than in construction names. Identify the construction family, convert it into yarn count, gsm, composition, weave, width and finish, and then check that the mill can prove each claim with a test method and a certificate. The difference between two quotes for the same poplin is usually not price negotiation — it is a difference in fibre content, weight tolerance or finish chemistry that was never written down.
The 2026 context supports that discipline. A USD 732.38 billion global fabric market and a 54.1% polyester volume share describe a category with wide substitution options, while Indonesia's USD 13.5 billion textile export base in 2024 points to a supply region with integrated capacity. For buyers, the practical leverage sits in documentation: a mill that publishes yarn counts, weights, compositions, testing standards and certification scope can be compared, audited and reordered. That is the standard to hold every candidate to, in Indonesia, China or anywhere else.
Request a Sample or Quotation
PT Golden Tekstil Indonesia develops woven apparel fabric from brief to bulk on a single campus in Kendal Industrial Park, Central Java — yarn dyeing, piece dyeing, digital printing and finishing in one process.
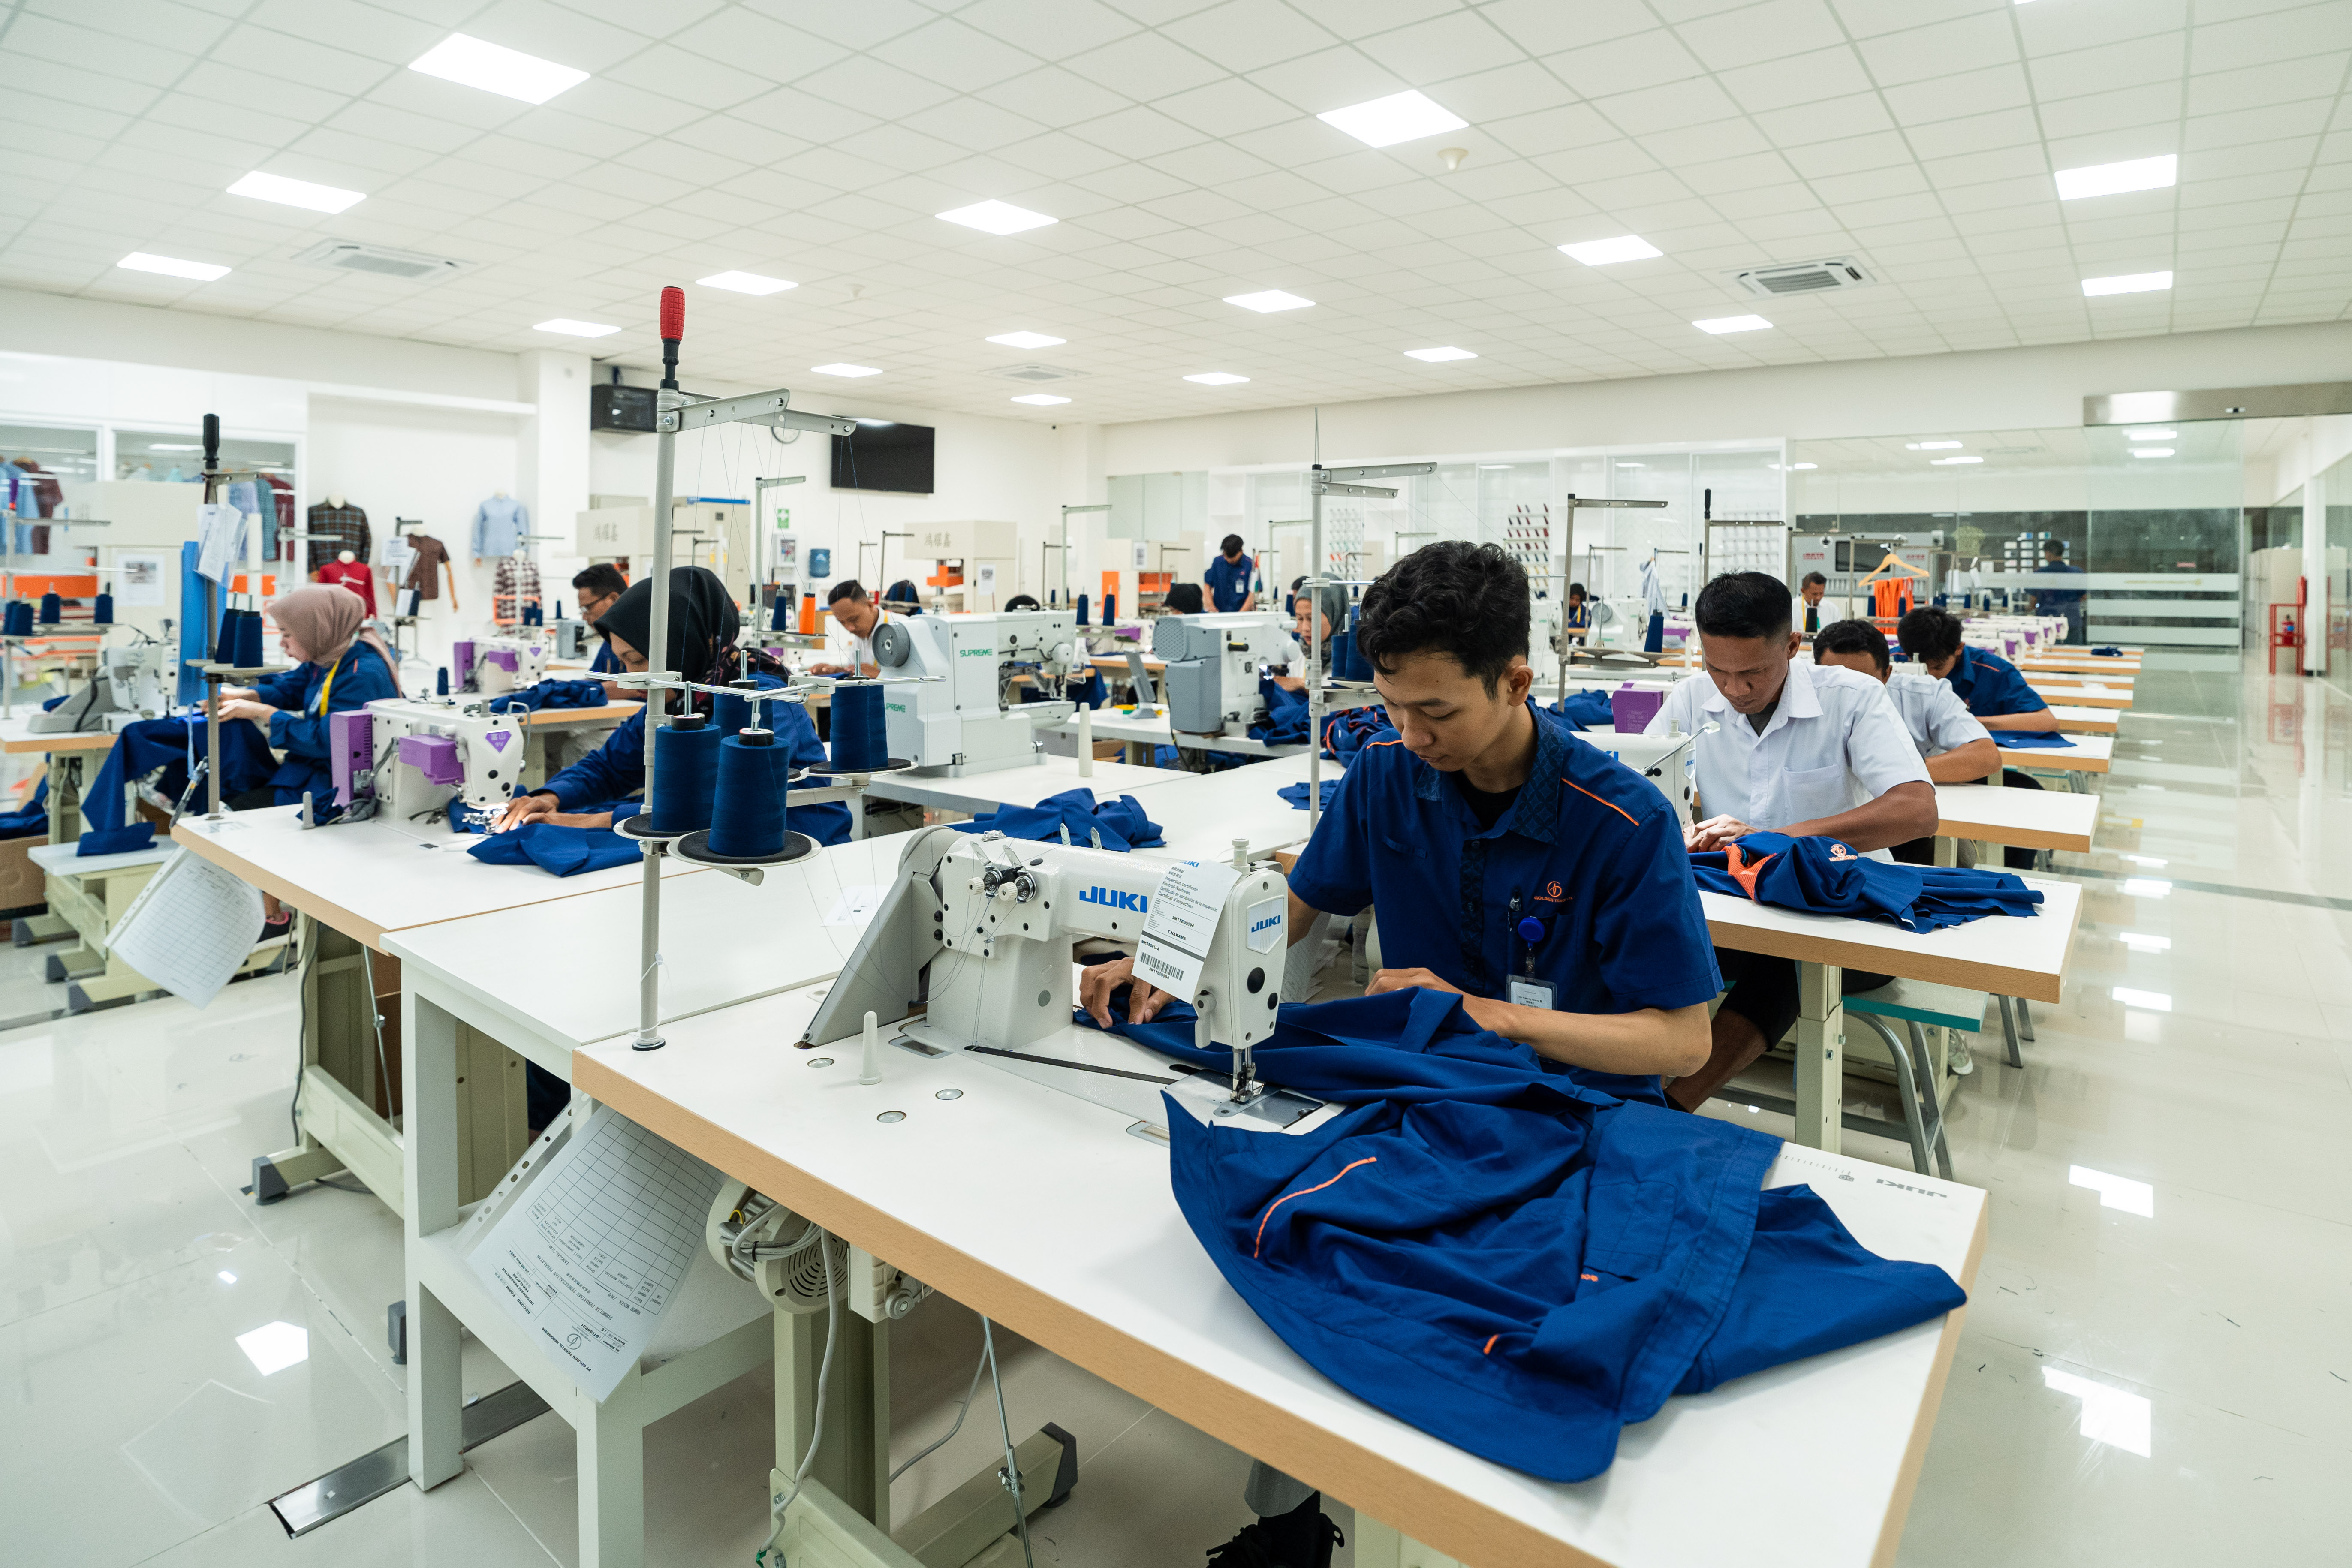
Send your specification and we will return a development plan, sample timeline and quotation.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.